Top Heat Exchanger Technologies for Global Buyers
Heat exchangers rarely attract attention until a process temperature drifts, energy use climbs, or production slows for cleaning. For global buyers, choosing the right equipment means looking beyond a catalogue image or headline efficiency figure. Heat Exchanger Technology spans shell-and-tube, plate, air-cooled, and other designs, each suited to different operating conditions. The best fit depends on the fluids, temperature range, pressure limits, available space, and maintenance plan.
Small details matter. A gasketed plate unit may allow quick access for inspection, while a shell-and-tube design can suit demanding duties and varied fluid streams. Air-cooled units can reduce reliance on cooling water, but their performance may change with ambient temperature and site layout. Fouling, corrosion, pressure drop, and spare-part availability deserve equal attention. These points are easy to underweight during purchasing.
This guide compares leading technologies through practical buyer criteria, including efficiency, materials, cleaning access, lifecycle costs, and supplier support. It also considers how certifications, documentation, and local service capacity can affect a project’s reliability. Specifications do not tell the whole story. Actual process data may be incomplete, and early estimates can be wrong; buyers should verify assumptions with qualified engineers and equipment suppliers before making a final selection.
Heat Exchanger Fundamentals: Thermal Duty, LMTD, and Overall U-Value
Heat exchanger sizing begins with a heat balance, not a catalogue. Thermal duty, Q, is the heat transferred per unit time: mass flow multiplied by specific heat and temperature change. U.S. Department of Energy’s Improving Process Heating System Performance: A Sourcebook for Industry reports that process heating accounts for nearly 50% of energy use in U.S. manufacturing. That scale makes small sizing errors worth checking. A measured flow rate and reliable inlet temperatures matter more than tidy assumptions.
The log mean temperature difference, or LMTD, represents the changing temperature gap between two streams. For counterflow equipment, calculate it from the two terminal temperature differences:
(ΔT1 − ΔT2) / ln(ΔT1 / ΔT2)
Overall U-value links duty, area, and LMTD:
Q = U × A × LMTD
U includes heat transfer on both sides, wall resistance, and fouling; its units are typically W/m²·K. A high U-value is not automatically better if the assumed operating conditions are unrealistic.
Check the smallest terminal temperature difference carefully. It can drive a much larger area requirement than a quick average-temperature estimate suggests. Still, the spreadsheet is only as honest as its inputs. Deposits, changing flow rates, and imperfect temperature readings can all shift actual performance.
Small gaps matter.
A conservative fouling allowance may be sensible, but excessive margin can also inflate equipment size and cost. DOE data provides context; site-specific measurements should guide the final design.
Shell-and-Tube Designs: Typical U-Values of 500–2,500 W/m²·K
Top Heat Exchanger Technologies for Global Buyers
Shell-and-Tube Designs: Typical U-Values of 500–2,500 W/m²·K
For shell-and-tube exchangers, 500–2,500 W/m²·K is a useful screening range for many liquid-service duties. Kern’s Process Heat Transfer and the GPSA Engineering Data Book describe overall heat-transfer coefficients as strongly dependent on fluids, flow, and exchanger design. Treat the range as a starting point, not a guarantee. Gas-dominated or viscous-fluid services may fall below it.
Water flowing through clean tubes can support higher coefficients than a sluggish oil stream. Condensation on the shell side may also raise heat transfer. Yet fouling adds resistance. A thin deposit can quietly reduce performance, even when the exchanger looks sound from outside. Check whether the quoted U-value is clean or fouled, and confirm its area basis.
For a quick review, compare the design U-value with the required duty, temperature difference, and available surface area. Then ask how the estimate handles fouling factors and flow rates. A spreadsheet can make assumptions look certain. They are not. The ranges in established engineering references help frame early decisions, but operating data and service-specific calculations should guide final sizing.
Top Heat Exchanger Technologies for Global Buyers - Shell-and-Tube Designs: Typical U-Values of 500–2,500 W/m²·K
| Service / Fluid Pair |
Typical Overall U-Value (W/m²·K) |
Common Shell-and-Tube Arrangement |
Typical Applications |
Selection Considerations |
| Water-to-water, relatively clean |
800–1,500 |
Fixed tubesheet or U-tube; one or more tube passes |
Cooling-water circuits, heat recovery, and process liquid heating or cooling |
Account for water quality, flow velocity, pressure drop, and fouling allowance. |
| Condensing steam-to-water |
1,500–2,500 |
Fixed tubesheet or removable-bundle design, depending on maintenance needs |
Process-water heating and steam-heated utility systems |
Provide for condensate drainage and non-condensable gas venting; verify steam-side pressure drop. |
| Water-to-glycol solution |
500–1,200 |
U-tube or floating-head design for services with notable temperature changes |
Chilled-water systems, heat-transfer-fluid loops, and industrial cooling |
Glycol concentration and operating temperature affect viscosity, heat transfer, and pressure drop. |
| Moderate-viscosity process liquid-to-liquid |
500–1,500 |
Floating-head or U-tube where thermal expansion or bundle access is important |
Process streams, product cooling, and heat recovery between liquid streams |
Evaluate viscosity at operating temperature, fouling tendency, materials compatibility, and cleanability. |
| Light hydrocarbon liquid-to-water |
500–1,000 |
Fixed tubesheet or floating-head, selected for inspection and cleaning requirements |
Hydrocarbon cooling and process-fluid temperature control |
Confirm phase behavior, allowable pressure drop, fouling risk, and applicable pressure-vessel requirements. |
U-values are indicative overall heat-transfer-coefficient ranges for preliminary comparison, not guaranteed equipment ratings. Actual values depend on fluid properties, flow arrangement, temperature, surface condition, fouling resistance, and design details. Gas-dominated services and highly viscous or heavily fouling fluids may fall outside the ranges shown; final sizing should use service-specific thermal and hydraulic calculations.
Gasketed Plate Units: Typical Liquid-Service U-Values of 1,000–5,000 W/m²·K
Top Heat Exchanger Technologies for Global Buyers
Gasketed Plate Units: Typical Liquid-Service U-Values of 1,000–5,000 W/m²·K
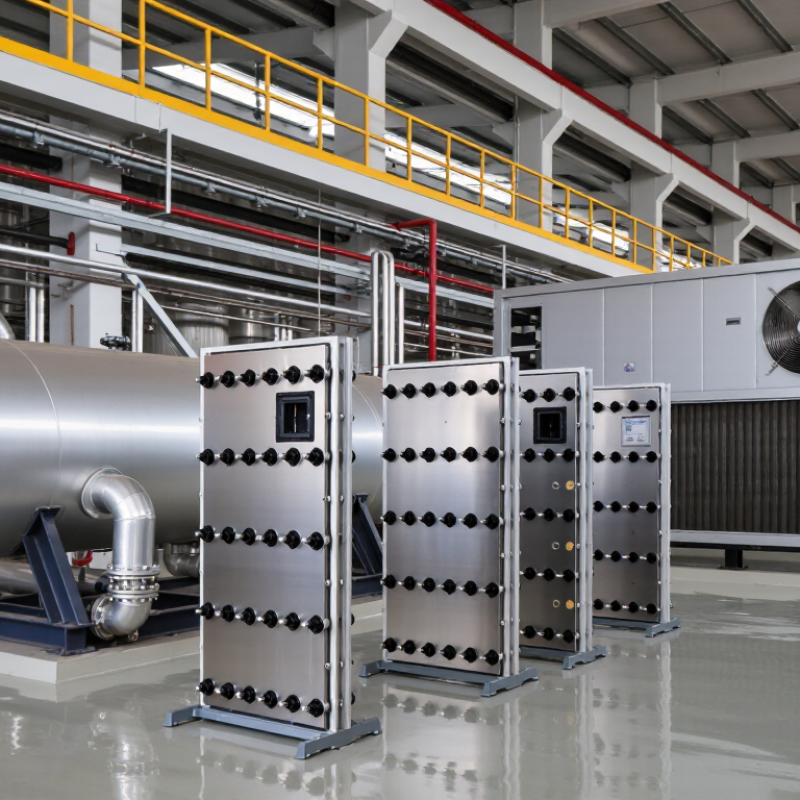
For liquid-to-liquid duties, gasketed plate units can deliver overall heat-transfer coefficients around 1,000–5,000 W/m²·K. This range appears in professional design references, including the VDI Heat Atlas and Kakac, Liu, and Pramuanjaroenkij’s Heat Exchangers: Selection, Rating, and Thermal Design. It is a useful starting point, not a guaranteed rating. Actual performance depends on fluid properties, flow arrangement, plate geometry, and operating conditions.
Consider a water-to-water duty with clean plates and turbulent flow: its U-value may sit toward the higher end. A viscous liquid, low flow rate, or fouling layer can pull it down. Small details matter. Engineers should confirm the design using inlet and outlet temperatures, flow rates, pressure-drop limits, and fouling allowances. The quoted U-value also depends on the area basis used, so comparisons between proposals need care. I would not size a unit from one headline number alone; real operating data are often incomplete, and that uncertainty deserves a margin.
Top Heat Exchanger Technologies for Global Buyers — Gasketed Plate Units
Typical liquid-service overall heat-transfer coefficient (U-value)
The bar shows the typical range of 1,000–5,000 W/m²·K for liquid service. Actual U-values vary with fluid properties, flow conditions, fouling, and exchanger design.
Compact Plate-Fin Units: Surface-Area Density Above 700 m²/m³
Compact plate-fin heat exchangers pack a large heat-transfer surface into a small volume. Some designs exceed 700 m²/m³, using thin plates and corrugated fins to create many closely spaced flow passages. That density can help when space and weight are limited, such as in modular process skids or equipment rooms with tight access.
The number alone can mislead.
Actual performance depends on fluid properties, flow rates, temperature range, and allowable pressure drop. Narrow passages increase heat-transfer area, but they can also be more sensitive to particles and deposits. That matters. A few millimetres of fouling may affect flow distribution and reduce duty.
Engineers should check the required temperature approach, pressure losses, material compatibility, and cleaning method before selecting a unit.
Not always.
The most compact core may not be the easiest to inspect or maintain. Ask for operating data and a clear design basis, including expected start-up conditions. A good review compares predicted performance with the process duty, rather than treating surface-area density as a guarantee.
Global Buyer Checks: ASME BPVC, TEMA, EN 13445, and Materials
Global buyers should check the governing design code before comparing exchanger quotations. ASME BPVC Section VIII covers pressure-vessel construction; TEMA adds mechanical requirements for shell-and-tube exchangers. EN 13445 addresses unfired pressure vessels. These documents are not interchangeable. Confirm the edition, design pressure, temperature, inspection scope, and required certification with the project’s destination market. IEA’s 2023 industry tracking puts industry at about 37% of global energy use. Small heat losses add up.
Materials need equal scrutiny. Match tube, shell, gasket, and weld materials to the actual fluid chemistry and operating temperature. Ask for traceable material certificates and confirm that heat numbers link to the parts installed. For chloride-bearing streams, for example, alloy selection should reflect concentration, temperature, and cleaning conditions—not just a generic “corrosion-resistant” label. Details matter.
Review corrosion allowance, weld procedures, and non-destructive examination records alongside the datasheet. A common gap is access: paperwork may be complete while inspection or tube cleaning remains awkward. Request drawings that show clearances, removable bundles, and maintenance access before approving fabrication. One more check. Ensure the code, material specification, and inspection plan agree; otherwise, a compliant-looking document package can still leave practical questions unresolved.